
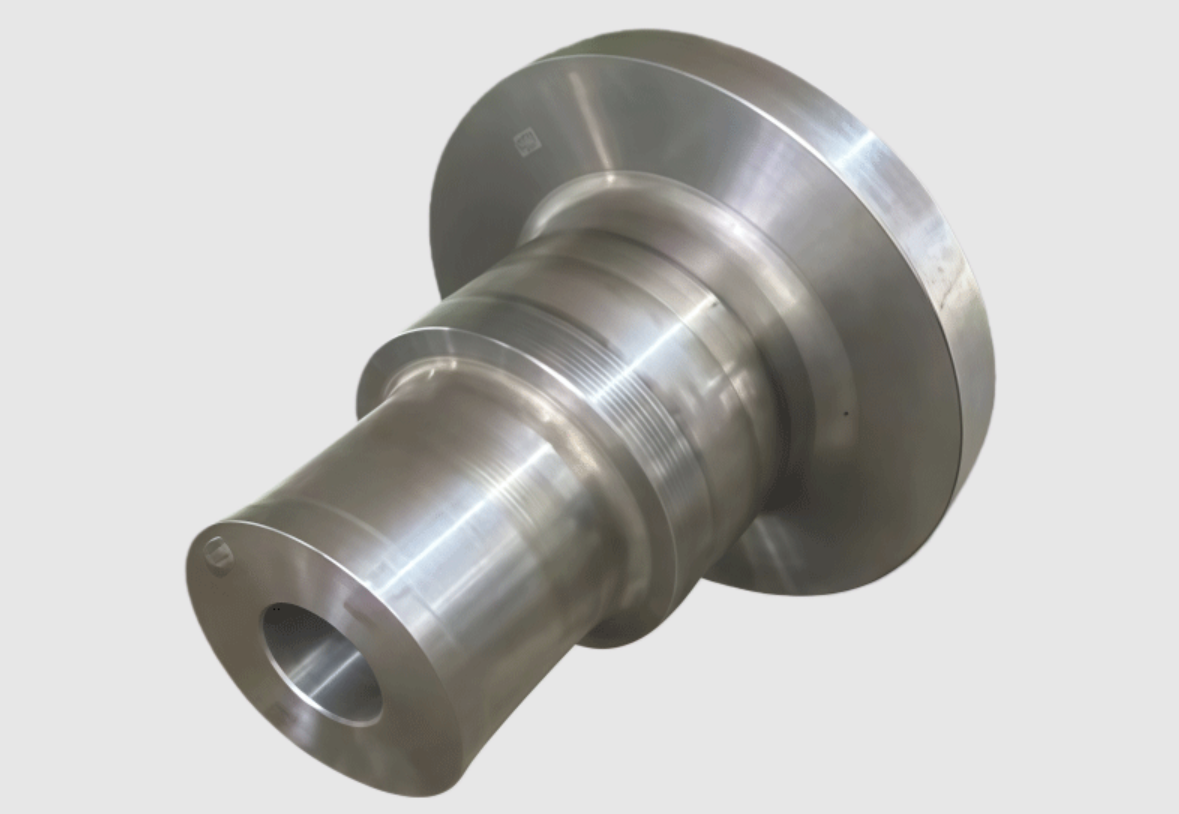
Sourcing Custom Forged Primary Sun Gear For Gearbox Solutions Provider: Key Specs Wind Power OEMs Must Verify

1. Core Banding Structure Control: Eliminating Micro-Segregation to Thwart Subsurface Cracking
High-power wind turbine operations expose planetary gear components to continuous, non-symmetric torque variations over decades of service. Under these severe cyclic loads, microscopic structural defects inside the steel matrix quickly expand into major macroscopic failures. Metallructural engineers identify severe alloy and carbide banding as a primary initiator of subsurface rolling contact fatigue. This phenomenon occurs during the initial ingot solidification stage, where vital elements concentrate unevenly within the cooling metal. If the subsequent hot working process fails to disperse these concentrations, distinct micro-structural bands develop across the component. These hard and soft alternating layers exhibit highly divergent mechanical properties under localized operational shear stresses. Consequently, early pitch-line delamination and micro-pitting develop rapidly along the boundaries of these weak microstructural bands. To eliminate this hidden operational risk, HONGDA HEAVY INDUSTRY utilizes advanced high-temperature diffusion annealing protocols. The production technicians subject the raw forged blocks to extended thermal soaking periods before starting the final shaping operations. This precise thermodynamic treatment forces the segregated alloying elements to diffuse uniformly across the entire crystalline matrix. As a result, the forged gear blanks achieve optimal structural isotropy, safely fulfilling the strict banding requirements of ISO 4967 specifications. Furthermore, eliminating severe segregation bands drastically lowers the risk of unpredictable hydrogen-induced cracking across the gear flank surfaces.
2. Hardenability Band Narrowing (Jominy Band): Guaranteeing Uniform Symmetrical Hardness Profiles
Achieving consistent wear resistance across every single gear tooth demands absolute uniformity during the final case hardening process. Standard industrial steel specifications often permit a relatively broad chemical variance within a single commercial alloy grade. However, these wide tolerances cause unpredictable hardness variations when the component undergoes deep induction hardening or gas carburizing. If the center of the gear achieves a different hardness level than the outer flanks, severe geometric distortions occur. To prevent this dimensional instability, wind turbine OEMs require a highly narrowed Jominy end-quench hardenability band. Managing this tight bandwidth requires absolute control over trace element additions during ladle furnace refining. Technicians carefully stabilize the specific ratios of chromium, nickel, molybdenum, and boron down to minute fractions. WUXI HONGDA HEAVY INDUSTRY CO., LTD tracks these metallurgical variations using automated chemical analysis systems. Furthermore, the facility deploys advanced heavy industrial equipment to execute highly precise thermal processing cycles. The Jominy end-quench test precisely measures this hardenability parameter by cooling a standardized steel sample under highly controlled water jet conditions. Specialized metallurgy labs plot these results to ensure the cooling response curve follows an exceptionally tight trajectory. Maintaining a narrow hardenability band ensures that the subsequent case hardening creates an identical, predictable martensitic layer across all profiles. This symmetrical material response permanently locks in the required gear geometry and prevents teeth deformation under load.
3. Fine Austenitic Grain Size Retention: Maximizing Dynamic Contact Fatigue Thresholds
The structural resilience of a heavy sun gear depends directly on the micro-scale boundary networks of its crystalline structure. Coarse grain formations drastically lower the total fracture toughness of low-alloy steel variants. Under repetitive tooth-impact cycles, large grain boundaries act as open pathways for rapid micro-crack propagation. In contrast, an ultra-fine grain structure deflects micro-fissures and absorbs localized kinetic energy safely. Therefore, modern wind power engineering mandates a consistent austenitic grain size of Grade 7 or finer. Achieving this ultra-refined microstructure requires a combination of smart micro-alloying and careful thermo-mechanical forging control. Small additions of aluminum, vanadium, or niobium form stable microscopic carbonitride precipitates throughout the alloy matrix. These dense particles act as physical anchors that pin the grain boundaries during high-temperature forging phases. HONGDA HEAVY INDUSTRY(WUXI HONGDA HEAVY INDUSTRY CO., LTD) masterfully balances these thermodynamic factors by utilizing highly controlled deformation speeds and precise finish-forging temperatures. This careful engineering ensures the material retains its fine grain structure during subsequent heat treatment. Offshore wind farms expose turbines to continuous aerodynamic turbulence and corrosive saline atmospheres, which accelerate material fatigue. Therefore, fine grain retention represents a vital defense line against sub-surface stress concentration points. Consequently, the finished components achieve maximum rolling-contact fatigue thresholds, allowing gearboxes to run smoothly for decades in severe offshore environments.
4. The 2026 Technical Audit Checklist for High-Power Wind Drivetrain Forgings
Procurement directors must apply a standardized validation matrix to verify the integrity of custom forged drivetrain parts. This technical checklist must transcend simple dimensional checks to focus on deeper volumetric and metallurgical indicators. First, inspectors must demand complete microstructural cleanliness data, verifying the absolute absence of large non-metallic inclusions. Second, the technical documentation must include multi-directional, high-resolution Ultrasonic Testing reports to confirm zero core porosity. Technicians must execute these critical ultrasonic scans in strict compliance with international frameworks like ASTM A388 or EN 10228. Third, the supplier must verify microstructural isotropy through comprehensive mechanical destruction testing on representative coupon samples. Obtaining independent validation records ensures that the component satisfies the uncompromising safety mandates of global insurance underwriters. Managing these multi-layered quality requirements becomes infinitely easier when dealing with a vertically integrated manufacturer. A single-source provider controls the entire workflow from the raw ingot receipt to the final precision pre-machining phase. This unified manufacturing control eliminates communication errors and prevents inter-process contamination between different vendors. Ultimately, securing a fully traceable component reduces supply chain friction and safeguards the capital investments of power grid operators globally.
Conclusion
In conclusion, the severe operational environments of modern megawatt wind turbines demand a new standard of forging excellence. Mitigating the risk of gearbox failure requires absolute control over micro-segregation, hardenability bands, and grain boundary structures. Traditional, loosely managed forging practices can no longer meet the multi-decade lifespan goals of modern offshore wind installations. Technical procurement managers must seek out verified engineering partners who prioritize absolute metallurgical data traceability. Implementing these precise material controls ensures reliable power transmission and lowers the total cost of asset ownership. To explore advanced manufacturing capabilities, evaluate metallurgical processing logs, and download international quality certifications, please review the official corporate portal at https://www.hongdaforge.com/.
HONGDA HEAVY INDUSTRY
HONGDA HEAVY INDUSTRY
Legal Disclaimer:
EIN Presswire provides this news content "as is" without warranty of any kind. We do not accept any responsibility or liability for the accuracy, content, images, videos, licenses, completeness, legality, or reliability of the information contained in this article. If you have any complaints or copyright issues related to this article, kindly contact the author above.
